HISTORIES
CASE
Zimmer provides a sure hold in cleanrooms
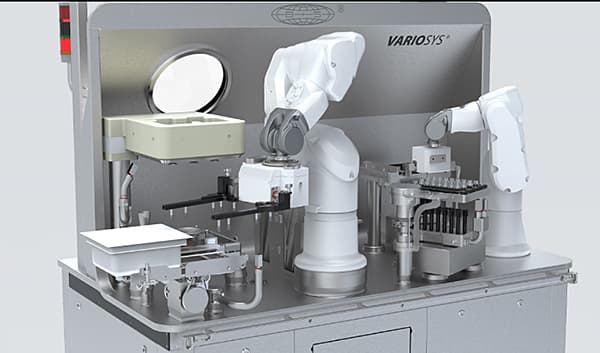
Pharmaceutical filling and packaging machine manufacturer Bausch+Stroebel (B+S) responded to the trend toward more automation and customization with its flexible VarioSys production system, a modular and sterile production system that fully automates filling and sealing of ampoules, syringes and vials.
The VarioSys system with a new machine module (DDM 9105) enables fully automated opening of tubs, denesting, filling and loading of RTU vials. For this purpose, they are transported by a pair of cleanroom robots equipped with grippers.
For the grippers, B+S is collaborating with Zimmer Group. Due to the cleanroom environment, a mechatronic gripper solution would be required.
Two grippers from the GEH6000IL series were selected from the extensive Zimmer Group portfolio. These long stroke electric grippers feature a servo drive with an integrated controller. Their brushless drive technology allows adjustment of force, position and speed. They also feature mechanical self-locking, preventing vials from falling in the event of power failure.
B+S also appreciated the fact that Zimmer Group was also able to respond very quickly to necessary modifications, such as flush connector and removable sealed enclosures. Furthermore, the gripper’s built-in IO-Link made it easy to transmit specific data, such as temperature measurement, position and cycle count.
Advanced Radial Riveting Process Control For Low Force Applications
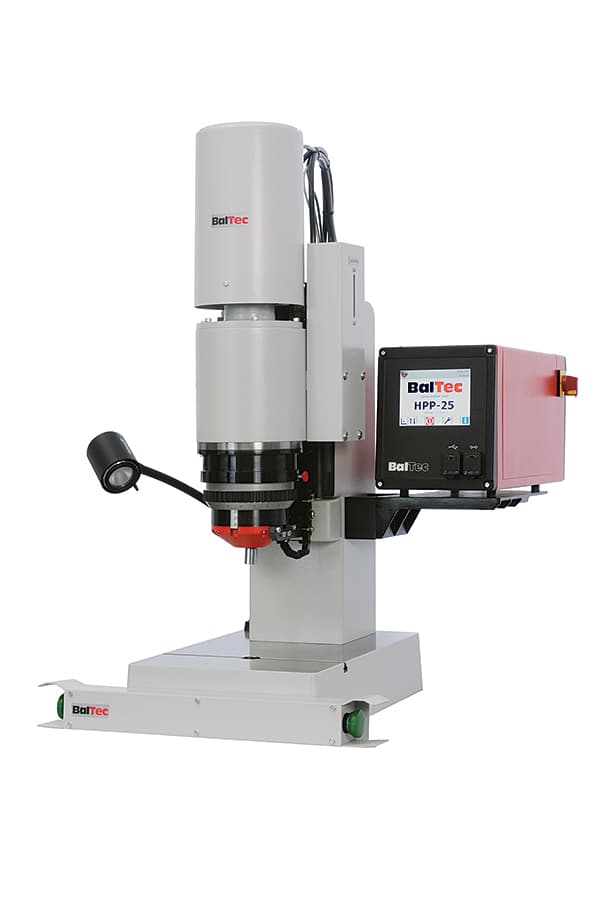
Baltec Corporation is pleased to introduce an advancement in radial riveting process control. With the HPP-25 process control, users can now control process variables in forming and assembly applications where the forming force is as low as .05-1.5 KN.
The HPP-25 process control package allows for the substitution of wide-tolerance, cold-formed rivets in applications that previously demanded close-tolerance machined rivets. Potential cost savings to the user are tremendous.
The HPP-25 package utilizes an Auto Compensation feature that allows for varying rivet heights of the rivet being formed. Real time rivet “stick-up” height data is sent to the controller where compensatory forming stroke, time and force criteria are generated and fed to your riveting machine to bring the rivet into a specified tolerance.
Real time recording of stroke, time, force, projection and head radius data ensures production uniformity.
Auto Compensation ensures higher levels of fastening integrity resulting in fewer scrapped parts and lower rework costs reducing the need for manual inspection and mechanical inline quality control.
ATI Robotic Tool Changers Enhance Assembly
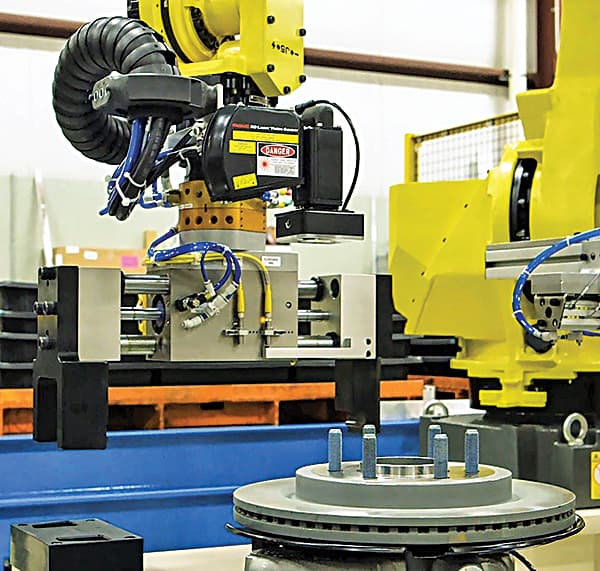
Edgewater Automation employed ATI Industrial Automation’s Robotic Tool Changers to enable existing robots to complete a variety of jobs; bringing dissimilar processes into a smooth automated system. The original line utilized six different operators with frequent disruptions as they moved in and out of the work cell to clear debris, orient parts and equipment, and execute tasks. Despite the use of robotic automation in each cell, robots and tooling performed singular tasks. The biggest challenge involved upgrading the application in the current footprint.
With ATI Tool Changers, one work cell now uses 3D vision technology and pick tooling to robotically inspect, orient, and select parts from a dunnage tray before mounting the parts to a swing arm assembly. Once complete the robot changes tools to remove the empty tray from the staging area and replace it with a new full tray. The application improvements free four of the operators to focus on specialized tasks such as programming, inspection, and quality; they reduce potential hazards while encouraging employee development. The unparalleled repeatability of ATI’s Tool Changers combined with the high efficiency of the robots ultimately leads to a more flexible application with reduced cycle time, longer production runs, and quicker processing.
Creform Corporation
(800) 839-8823
SCsales@creform.com
www.creform.com
Creform anti-static mobile flow rack
Creform Corporation has designed and built a mobile gravity-fed, anti-static flow rack. The flow rack features three levels for product presentation and each level features five lanes. This guarantees first in-first out (FIFO) inventory management. Each of the five lanes features a separator so that the boxes are contained within the lane. Further, each lane features three Creform’s electrostatic- discharge (ESD) high-quality skatewheel conveyor rollers. These provide for a smooth flow of product.
The flow rack’s dimensions are 140” W x 43” D x 54” T and is designed to hold up to 750 lb. It is built with ESD plastic-coated “black” pipe and nickel-plated metal joints. It features 12 heavy duty stem casters that aid in moving the structure for housekeeping or relocating. Four of the casters feature brake capability.
As with all Creform flow racks, higher capacity, sizes and configurations are possible. A wide variety of pipe colors are available for non ESD applications, and accessories can include information sheet holders, label holders, tool storage, hooks to hang tools and other supplies. They are available as a kit or an assembled structure or in the component form for a complete DIY solution.

Wire Harness Benches Increase Production.
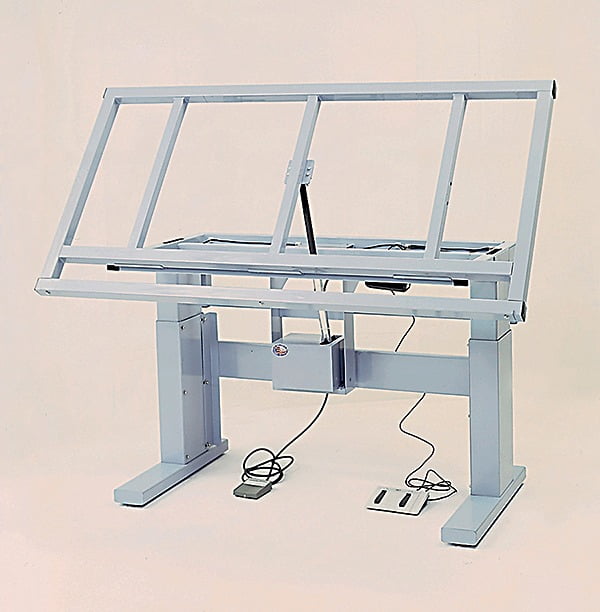
Tolerances have to be consistently tight when you’re assembling wire harnesses for a jet fighter – 1/8 of an inch over 32 feet to be exact. Workbenches that can’t accommodate such tolerances would be, well, intolerable.
That’s the problem that a jet manufacturer faced when they determined that they needed to upgrade their facility. They were using pieces of plywood on A-frames for the assembly. This not only affected tolerance levels but also led to stress, strain and fatigue.
The jet fighter manufacturer found a company that could deliver what they were looking for in Proline. A leader in ergonomic workbenches. A company renowned not just for its rugged, technologically advanced workbenches, but also for its ability to “think on the fly” and produce, application-specific solutions, Proline met all of the jet manufacturer’s specs.
Thanks to the range of easy vertical movement provided by the Pro-Line benches, along with tilt, all sections of the wire harness are always within easy reach. Since this initial installation, this jet plane manufacturer is currently in the process of expanding its operation with additional Pro-Line workbenches. Clearly they are more than satisfied that they have harnessed such precise, ergonomically sound and productivity-enhancing workbench solutions.
Lanco Integrated
(919) 572-2705
sales@lanco.net
www.lancointegrated.com
When Lanco Integrated needs an accurate gripper with repeatability and a compact size, they turn to SCHUNK!
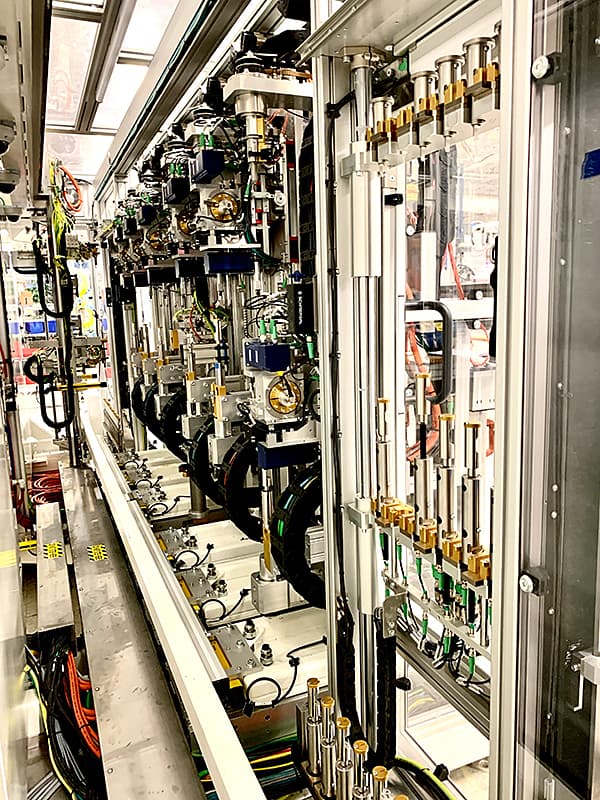
Lanco Integrated is updating their very successful set of suture machines; the original machines were developed over 10 years ago and are still performing well. This latest revision allows the customer to load and unload product in parallel with the barbing process, and provides automatic changeover to accommodate different suture lengths and gages.
The team faced a number of challenges dealing with one of the “densest” systems they had produced; the system has intense wiring so cable management and routing had to be carefully considered. Additionally, a safety scheme was needed to allow operators to access the machine for loading and unloading while it is running.
The team at Lanco Integrated did not have to worry about which gripper supplier to choose. They have been working with SCHUNK, who makes the largest range of standard gripping components on the market, for several years, and knew that the compact and reliably repeatable KGG grippers were the right choice for this machine design.
According to one Lanco representative, “Lanco has used SCHUNK grippers for many years, because they just work! This system required accurate repeatability, and SCHUNK’s KGG is a small compact gripper that works very well for handling a size 1 to 4/0 suture thread.”
Fusion, Inc.
440-946-3300
www.fusion-inc.com
Fusion, Inc. – your ONE SOURCE for all of your brazing and automation needs!
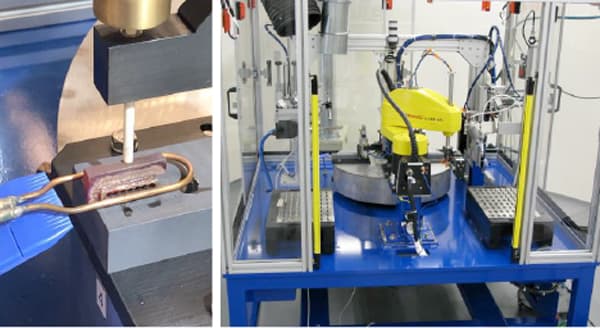
Fusion, Inc., an Ohio-based developer and manufacturer of brazing pastes and automation equipment, was approached by a tooling company with an interesting challenge. Could Fusion, Inc. assemble and braze a cutting tool consisting of two parts – a diamond matrix cutting segment, brazed to a base mount made of an alloy of iron, nickel and chrome? The tooling company then takes these finished assemblies and mounts them to belts used to cut stone in quarries.
This program presented a number of challenges. First, there was the production rate, which was 60 pieces per hour. It sounds simple, until you realize the brazing and cooling times were both lengthy in time. Next, there was the automation of the assembly. The two parts formed a butt joint. The base mount had to be laid on top of the cutting segment, then held in place in a repeatable way. Finally, the two parts had to be brazed, cooled, and then removed from the assembly automation.
Fusion, Inc. was up to the challenge. Drawing from a vast history of automation designs, it was decided a SCARA robot and induction brazing, all contained in a rotary brazing station, offered the most cost-effective solution. The automation was built, and the result was a reliable brazing system, which provided the tooling company with the parts they needed at a production rate that met their requirements.
Fusion, Inc. – your ONE SOURCE for all of your brazing and automation needs!
Sankyo Automation
937-498-4901
www.sankyoautomation.com
Rotary Positioner Decreases Cycle Time
A manufacturer of glass panels for LCD displays needed to decrease the cycle time of a grinding application in order to meet production demands. Between each grinding pass, the glass panel needed to be indexed 90 degrees both accurately and fast.
The previous machine design used a Direct Drive motor to position the glass panel. The DD motor was capable of indexing the 7 kilogram mass 90 degrees in 0.4 seconds with an indexing accuracy of ±5 μm. They were unable to improve the indexing time beyond this due to the unsatisfactory settling time of the DD motor.
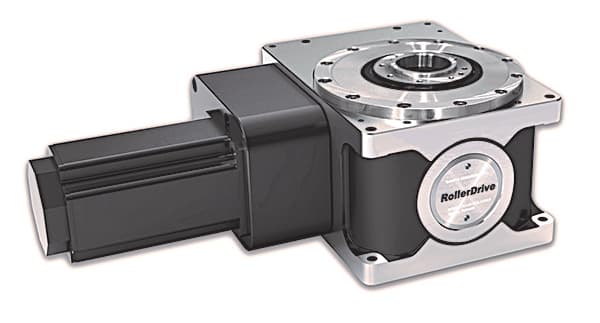
Sankyo recommended using their RollerDrive technology in the form of the RU Series rotary table. The unique RollerDrive technology uses preloaded roller followers on the unit’s output to completely eliminate backlash. The RollerDrive technology allows the RU Series to benefit from the robustness that gear reduction provides, while still maintaining accuracies that are on par with DD motor technology.
The switch to RollerDrive technology was a decrease in indexing time to 0.2 seconds along with improved positioning accuracy to less than ±4 μm. With three indexes per panel, the cycle time was reduced by 0.6 seconds and an efficiency gain of 12% was realized.
ViscoTec America Inc.
770 422-4281
770 422-0265
sales@viscotec-america.com
www.viscotec-america.com
Optimized Sealant Dispensing for Chemetall
At ViscoTec, it is standard practice to reproduce and simulate processes and projects in the in-house technical center and to verify them together with the customer or the respective material manufacturer. For example, joint trials were carried out with the material manufacturer Chemetall using the Naftoseal MC-780 B-2 sealing material, which is well known in the aerospace manufacturing industry. It contains tiny hollow polymer spheres and is therefore compressible – which is particularly challenging from a dispensing point of view! Using a real component from a passenger aircraft, an application was recreated to gain further experience and identify potential challenges.
Not only was the material application the focus of the dispensing tests, but also the inspection of the properties of the mixed material. An analysis of the dispensing results was therefore carried out together with Chemetall. Heinz Burock, Aerospace Application Technologies Manager at Chemetall on the results: “Previously unattained precision of the specified mixing ratios for all dispensing quantities, as well as scalability of the system from cartridge filling to the application of the mixing head on a robot with large cartridge supply, are the outstanding features of this technology.”
Electric Tools for Electric Vehicles!
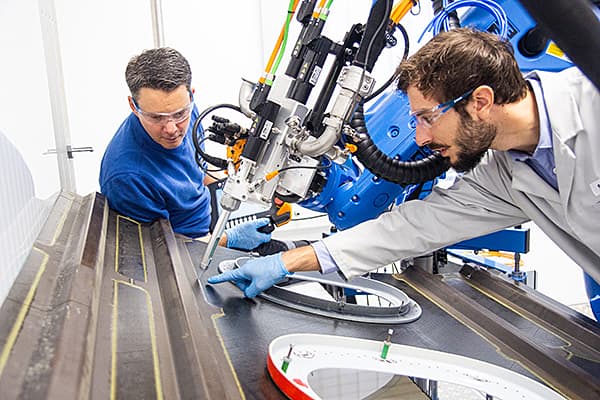
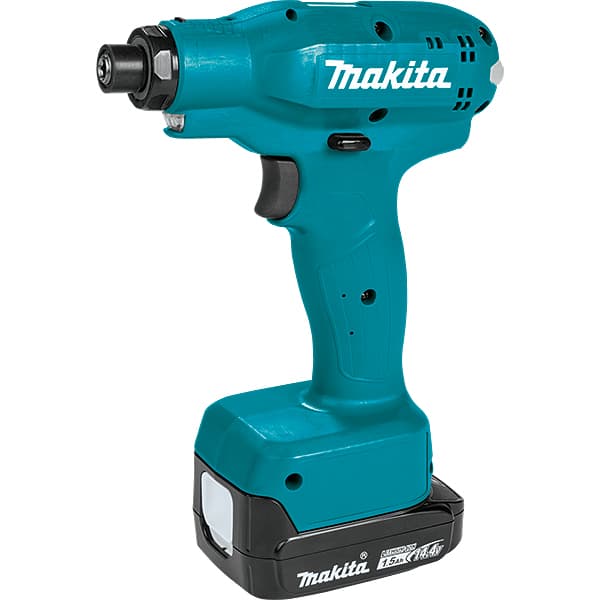
Realizing the energy savings from electrically powered equipment is not a new concept, so it is no surprise that many of today’s electric vehicle (EV) manufacturers look to battery-powered tools FIRST for their production and assembly needs.
The most recent example was when, earlier this year, a brand-new mid-west EV company purchased over 500 cordless tools for their assembly line. Instead of using traditional pneumatic tools, this manufacturer partnered with Makita for all their cordless assembly tooling. Understanding their energy cost savings, ergonomic benefits, and the advanced technical solutions that Makita tools offered, they recognized Makita as the superior choice for their capital investment. Their $500,000 investment paid off immediately with a 90% reduction in operational cost from lower energy consumption, and a return on investment within 6 months. Further, they eliminated potential safety and trip hazards from air hoses and realized huge ergonomic benefits and increased mobility. In addition, quality standards increased, as Makita’s precision torque tooling is proven to be more repeatable than pneumatic tooling.
Makita continues to provide solutions to the ever-changing production environment. As assembly facilities seek out new technologies to ensure Lean Manufacturing principles, Makita will continue to offer quality tooling that exceeds expectations for our strategic partners.
Durofix Inc.
909-980 3323
info@durofix.com
www.durofix.com
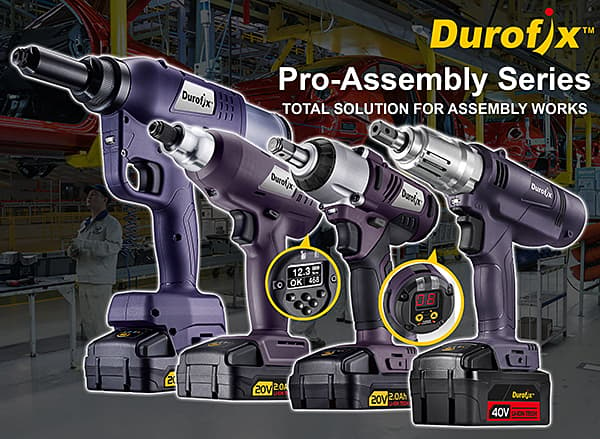
Durofix Precision Fastening Power Tools
With over 30-year in power tools industry, Durofix and its parent Mobiletron is extending product portfolio to precision fastening power tools for automobiles, aerospace, infrastructure and construction industries.
As a manufacturer ourselves, we fully understand that manufacturing operations always struggle to achieve the best of Quality, Efficiency and Cost.
Durofix Pro-Assembly Series power tools are cost-effective, efficient, high precision fastening solution for all professional assembly operations. From Brushless Mechanical Impact to Hydraulic Oil Pulse and Transducerized Sensing, the series offer a wide torque range, from 1 Nm to 700 Nm, state-of-the-art technologies for various applications and production setups.
Precise Torque Controls, achieved by Hydraulic Oil Pulse and Transducerized sensing technologies and Multi-Stages Electronic Torque Control, delivers error-free production quality.
What’s more? Selected models also equipped with built-in wireless data communication function for plant manager to oversee and record real-time operation details through iOS devices or existing PLC system.
The ever growing product family is your best choice of precision fastening.
Motion index Drives
877-978-1830
info@mid.us.com
www.motionindexdrives.com
RT400-Flex for Aerospace
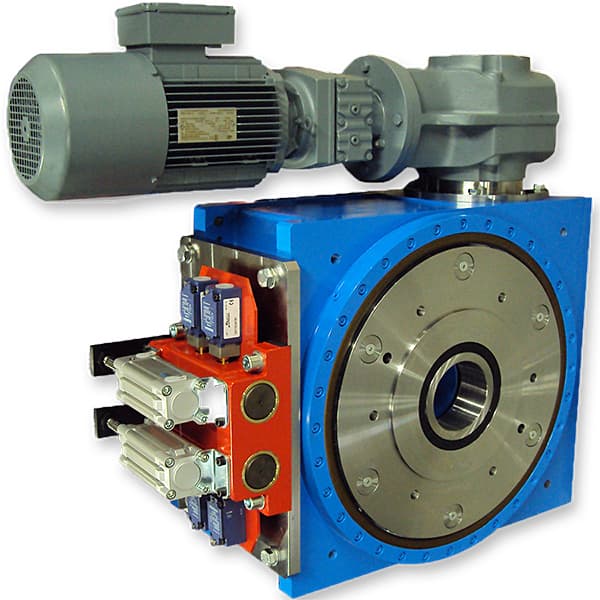
An integrator building a system for Boeing Aerospace Company had a strict requirement for a “Zero Backlash” rotation system for positioning of reverse thruster part as it was being assembled. The
reverse thruster and carriage had a total load of 4000 lbs with a payload of a physical size of 140”x 80” x 60” and a 5:1 safety factor. The positioning system had to be manufactured to allow for slight misalignment and equipped with a safety locking device.
The RT series 400-Flex trunnion is equipped with a programmable barrel cam which fit the end customer’s specifications. The barrel cam/cam follower mechanism operates in a preload condition allowing for a true “zero backlash” operations. Our case hardened barrel cams (5 mm depth) and needleless cylindrical cam followers allows for maximum torque to be generated. The custom floating bearing assembling on the tail end, opposite of the RT400-Flex unit allowed for slight misalignment. The tail end bearing assembly was able to float in and out to accommodate any structural size differences that may occur from expansion and contraction. We equipped the RT400-Flex with a safety lock out device and custom output flange to give Boeing plenty of option to engage the safety lock-out device at multiple angular positions.
WEISS North America, Inc.
888-WEISSNA (888-934-7762)
info@weissna.com
https://www.weiss-world.com
Highly Accurate Assembly Requirements Achieved
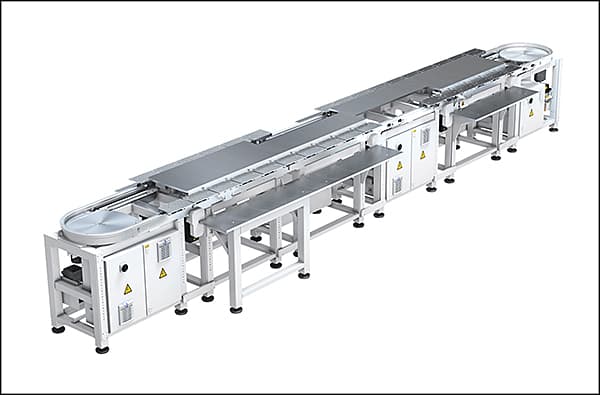
Recently, a customer in the agriculture industry reached out to WEISS North America regarding the development of a highly accurate assembly system with a production rate of 1800 PPH and a cycle time of two (2) seconds per assembly. This particular application involved several processes, such as assembly, filling, dispensing, spinning, laser marking, and pressing of sprinkler assemblies.
After reviewing the requirements of the application and considering the various multiple parts and process time requirements, WEISS North America was able to develop and deliver a custom solution that is built around their proven WEISS LS280 Linear Transfer system. To overcome the challenge of the customer’s varied process times, the system was designed with different cam pitches. The 2 second cycle time was achieved by utilizing highly accurate and fast WEISS HP pick and place units and HN & HG linear actuators.
WEISS provided the complete solution including a custom chassis surrounding the LS280 and all electrical enclosures with cable management for all the direct drive components. The complete system operates on WEISS Application Software (WAS-2).
Schleuniger, Inc.
603-668-8117
Toll Free Technical Support: (877) 902-1470
Sales@schleuniger.com
schleuniger.com
Maximizing Quality and Improving Process Times
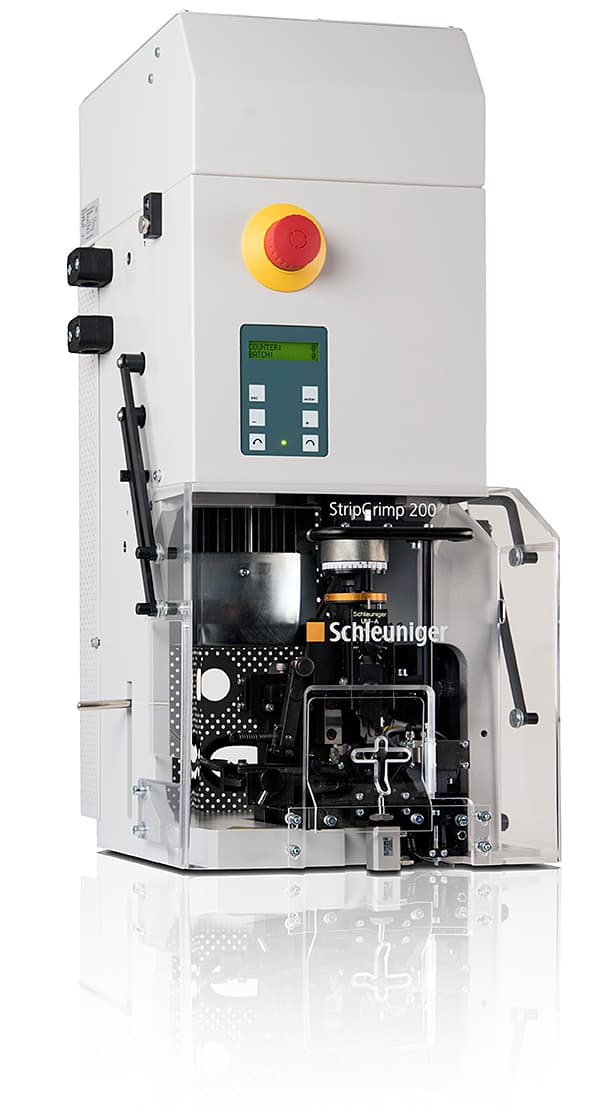
Total Quality Instrumentation, Inc. (TQI) located in Cookeville, TN., manufactures a variety of products that support the automobile development and heavy trucking industries. In 2015, TQI purchased their first Schleuniger machine. Prior to that, most of their applications were done by hand. Since then, the company has purchased several more machines for various applications.
TQI must be able to precisely cut and strip to length, a variety of wire sizes and colors. According to TQI President Richard Grogan, “The accuracy of the MultiStrip 9480 cut and strip machine prevents recuts and the durability of the rollers is unmatched. And because your software integrates with Microsoft Excel, we are able to send the production list to the machine where the operator can follow simple instructions to load the material, run the product, and rapidly move to final assembly.“ Consequently, TQI estimates a 40-50% decrease in their overall process time! “The accuracy of the StripCrimp 200 is unparalleled,” says Grogan. “It strips and crimps the wire to perfection.”
It is clear to Total Quality Instrumentation, that Schleuniger helps them provide the highest quality products and services. Grogan adds, “Schleuniger solves a problem, instead of making one.”
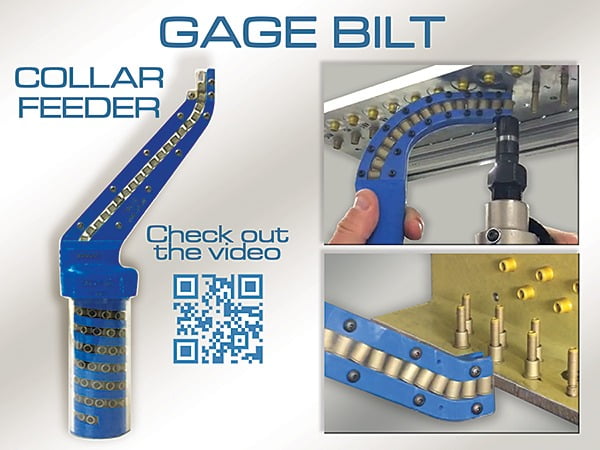
Increase Productivity and Control F.O.D. with GAGE BILT’S Collar Feeder.
Gage Bilt Inc., located in Clinton Township, MI, is celebrating its 65th Anniversary as a manufacturer of Aerospace and Commercial blind rivet and lockbolt installation tools. Gage Bilt is known for, not only the most robust tools on the market, but also its ability to innovate and solve problems for customers.
A leading Aerospace company was experiencing ergonomic, speed, FOD and major safety issues while installing a two piece fastener known as a lightweight lockbolt. There were three main factors that we needed to address. First, a normal installation forces the operator to position the collar with their fingers while using an installation tool with over a 6,000 pound pull load. Consequently, operators were injuring their hands and fingers. Second, while positioning the fastener, operators would often drop the collars into the aircraft causing FOD. Third, the time it took an operator to orientate the collar in the proper position was slowing the installation process. Considering these issues, Gage Bilt began to innovate.
The result was Gage Bilt’s newly patented GB5500 Series Collar Feeder. The GB5500 acts as the operator’s fingers while keeping their hands at a safe distance, improves ergonomics, controls FOD, positions the collar in the proper direction and sped up the installation process for our customer! It’s simple, lightweight and can be designed for many different types, shapes and sized collars. The profile can be altered to fit specific applications no matter what direction or orientation.
Watch a video on our website and contact Gage Bilt with any inquiries.
Starline
724-597-7800
info@starlinepower.com
www.starlinepower.com/applications/industrial
Eliminate Electrical Constraints
with Flexible Power
When the company began its transition into manufacturing in 2006, Winar Connection discovered its building was not conducive to production and constructed a brand new, 80,000 sq. ft. facility.
As the company grew, implementing new state-of-the-art equipment posed many challenges, including having to decide where to place the equipment, and then contracting an electrician to hardwire it in place. These changes could take up to eight weeks to implement.
Winar knew it had to find a solution to avoid the electrical flexibility constraints it had experienced in its old building. Winar chose the 100 amp Starline Track Busway product because it needed a system that could grow with the company.
Using Starline, the same workstation rearrangement that used to take up to eight weeks was reduced to a single day. Where previously the best way to move hardwired equipment was by using extension cords - a significant safety hazard – by utilizing Starline, Winar could simply unplug a plug-in unit, safely move it to its new location, and have equipment ready within 15 minutes.
Ultimately, Winar can configure its production layout for operational efficiency and can rest assured that access to power will not bottleneck future changes.

Reduce Scrap by 80% with Cross Thread Prevention
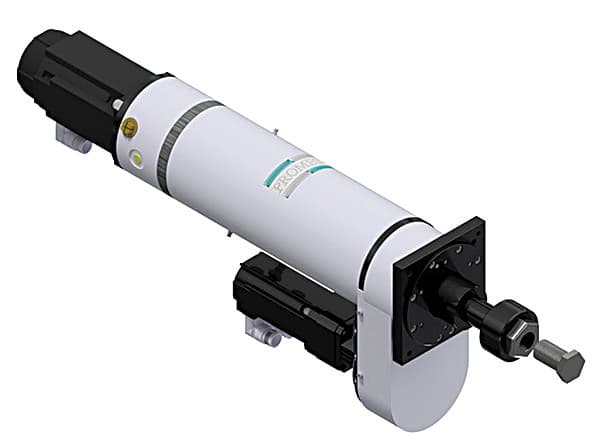
The customer needed to thread two sub-assemblies together and torque to a specific value. Using the combined technology of closed-loop press and torque movements in our REMAP and the flexibility of our UltraPRO Controller, Promess was able to help this company retrofit our product into their existing station with little modification.
First, the press moved the part that was nested in spring-compliant tooling. Next, we would gently apply pressure to the part in the range of 100lbs of force with the press axis. We then rotated the torque axis counterclockwise. During this movement, we collected the press force-over-rotation data which was essentially measuring the force on the part while rotating. Using this data, we looked at the lowest point of force and saved that position. This position indicated where the threads “clicked” together. Rotating to this known position, we knew we could begin rotation in the clockwise direction and on to torque the unit to its final specification.
Promess was able to reduce the scrap rate of the part by over 80%, cut the leak test failures to almost nothing, and the system paid for itself within the first 9 months of use. Additionally, the overall cycle time was reduced by about 10 seconds.
Making the Switch to Ujigami
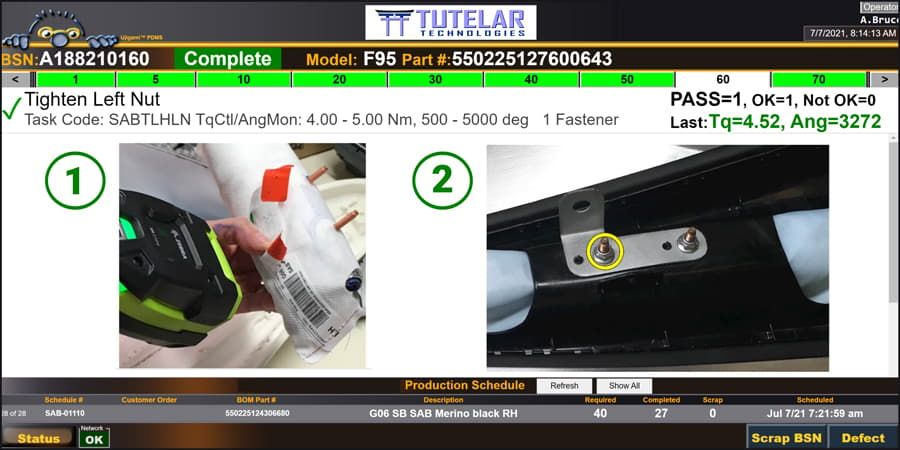
An Automotive Seating supplier was having issues with the rigidity of their MES system forcing them to scrap good airbags when the larger finished good had any sort of defect, including appearance issues. This supplier was throwing out thousands of dollars of quality components every day, until they switched to the Ujigami Product Directed Manufacturing System (PDMS). With Ujigami’s active control and intelligence, first time quality immediately improved and lowered the occurrence of defects – but when defects occur, Ujigami knows what part is compromised, and which parts can be re-used in another finished good.
The changeover was simple, with an Ujigami team member taking existing work instructions and importing them into a new Ujigami configuration. The process was completely turn-key, and after a short period of off-day testing production resumed on Monday at full capacity.
This seating supplier is now able to utilize Ujigami’s flexible architecture to do continuous improvement and make significant line changes without programming. They also utilize Ujigami’s Scheduling module to dramatically improve their scheduling mix and changeover process to reduce waste – another immediate return-on-investment.
For more information including how Ujigami can make a difference at your facility, please email us at sales@watchover.us
Tutelar Technologies Inc.
905-331-6808
sales@watchover.us
www.watchover.us
Emerson
1953 Mercer Rd
Lexington, KY 40512
859-254-8031
customer_us_lex.aventics@emerson.com
Emerson.com/AVENTICS
Smart Pneumatics Optimize Palletizing Performance
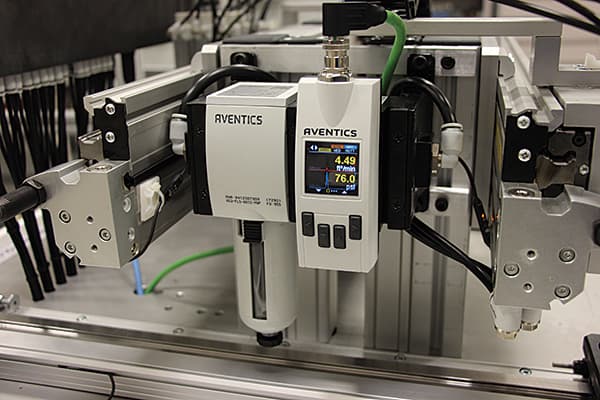
High-speed, automated bulk palletizing systems influence the overall equipment effectiveness (OEE) of a facility’s entire packaging line. To maximize customer OEE, a leading palletizing company worked with Emerson to digitally transform its high-speed bulk depalletizer and palletizer by integrating machine health monitoring capabilities that help operators diagnose potential issues before they become big problems. Emerson added smart pneumatics, edge computing and an IIoT software platform that provide real-time, actionable data about equipment condition and performance.
This comprehensive solution monitors critical motion and pneumatic system parameters that can pinpoint irregularities. Emerson’s AVENTICSTM ST4 cylinder velocity sensors notify operators when components perform below critical thresholds, while AVENTICS AF2 Flow Sensors diagnose leaks and excessive consumption across the compressed air system. Easy-to-read displays and alerts make it simple for the right personnel to respond to issues quickly and efficiently.
Emerson’s PACEdge 2.0 IoT platform running on the PACSystems™ RXi2 Edge Computer brings these data sources together. The interoperable, scalable platform provides real-time data access, historical performance tracking, visualization and analysis of the smart pneumatics system. The complete system helps customers improve energy efficiency, reduce unplanned downtime and lower costs, increasing the value the palletizing company provides while supporting the digital journeys of all.
Consult an IIoT Expert
Durability Passed with Hydraulic Pulse Tools
Challenge — All manufacturers face the task of finding an ergonomic assembly tool with torque control; minimal torque reaction; low operational costs; and improved uptime.
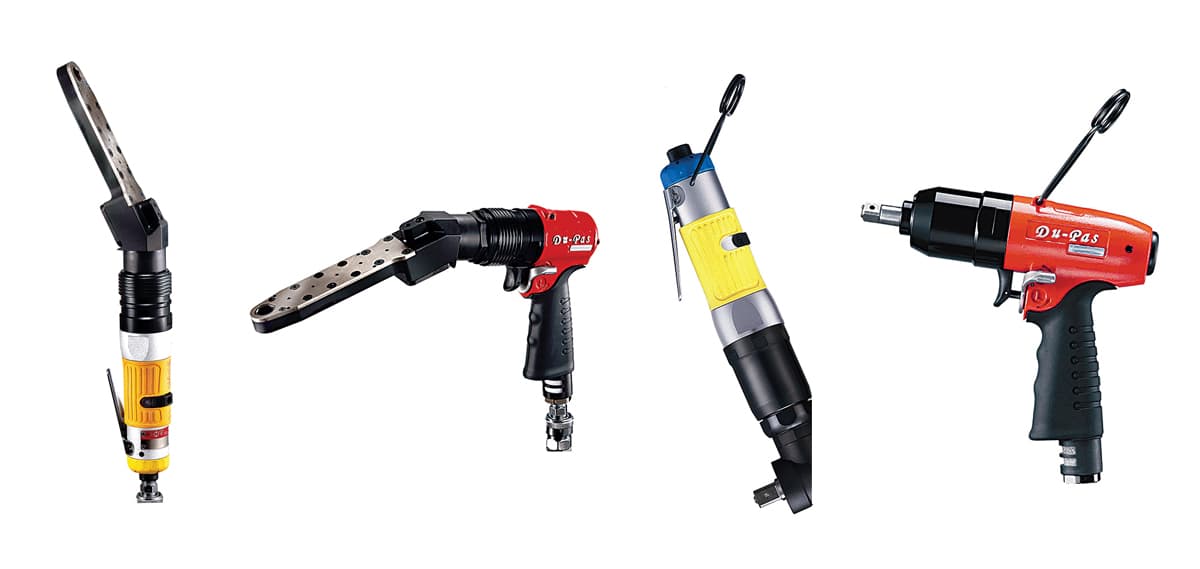
The discontinuous drive feature of Hydraulic Pulse Tools apply torque in increments rather than one continuous effort; thus, eliminating torque reaction to the assembler. The ergonomic and torque control features of this tool configuration make this the best relative to low Total Acquisition Costs. However, this tool type is characterized to have higher associated operational costs.
An automotive manufacturer in the southeastern U.S. had tried nearly every brand of hydraulic pulse tool on a very challenging application with high cycle rates. Only one brand would operate in production for one week before service was required. While this weekly service interval was not satisfactory, the automotive manufacturer had accepted this as a standard based on their challenging application.
Solution — In looking for a more durable discontinuous drive hydraulic pulse tool, the automotive manufacturer tested a Du-Pas TDIS Series hydraulic pulse tool.
Result — The DuPas TDIS Series exceeded their expectations. The robust external design of the housing coupled with the internal double sensing pulse mechanism resulted in increasing their uptime by 300% from all other tool O.E.M.s they tested. The TDIS Series proved to be a robust, low Total Cost of Ownership solution!
Durability Passed!
High Torque, High Throughput, Multi-Driver Assembly Cell
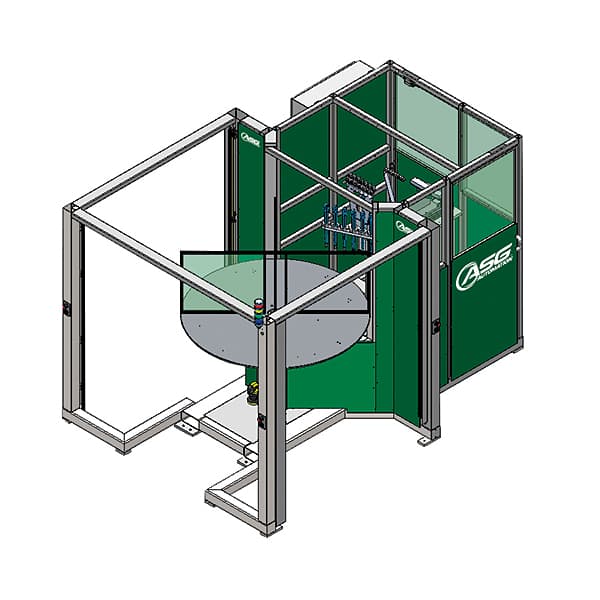
A customer recently approached ASG Automation with a challenge – to fabricate an industrial assembly that had several critical requirements: less than a 30 second cycle time to fasten 20 nuts at over 50 lbf.in. A custom ASG AX-30 turntable system fit the bill.
The customer’s current process was to build the assemblies by hand which resulted in a number of quality problems like missing or under torqued nuts as well as a lengthy cycle time. Needing to make an improvement, the customer came to ASG Automation for a solution.
This particular AX-30 system utilized a 4 position indexing table with multiple pneumatic nut drivers. The open design of the system allowed for operators to load the components from two of the 4 stations, the 3rd station completing the fastening of the nuts to the assembly, and the 4th station for completed part removal. Not only did the system achieve a highly repeatable torque, but ASG Automation was able to cut almost 10 seconds from the customer’s 30 second cycle time request improving their output by 33%!
ASG, Division of Jergens, Inc.
Products & Solutions for Assembly
888-486-6163
Fax: 216-481-4519
www.asg-jergens.com
ALM Positioners, Inc.
309-787-6200
sales@almmh.com
www.almmh.com
ALM Positioners Heavy Duty Solutions for Heavy and Wide Equipment
ALM Positioners, Inc. takes pride in providing positioning solutions for multiple manufacturing industries. Komatsu Mining Corp’s overall goal in looking for positioners was to improve safety and productivity.
Joe Nara of Komatsu states, “Before we bought the positioners, it would take 3 to 4 guys a minimum of 30 minutes using cranes to turn the frames. It now takes about 4 minutes to lift the frame to the top and rotate it 360 degrees and back down. The positioner keeps our cost down and having a high-capacity positioner means that it can be used with the wide range of frames with which we work. The guys out in the shop feel much safer using the positioners instead of a crane. Plus, using positioners frees up the overhead crane for other parts of the facility, and that in itself is another bonus. We are viewing productivity improvement savings around 100 hours per frame. We love bringing our customers into our facility to show them how the frame is coming out; they are instantly impressed. When they come in, they see the benefits of the positioners, particularly that their frames are getting completed faster. The support and service have been timely. Overall, I am very impressed and have no complaints. I am excited to continue working with ALM in the future.”
ALM’s Heavy Duty (HD) line of positioners ranges from 75,000 LB - 125,000 LB.
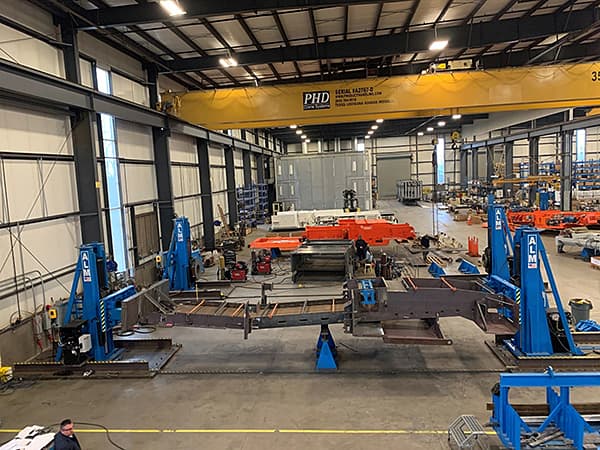
ABB Moves EMH NOMAD Easily. Reliably.
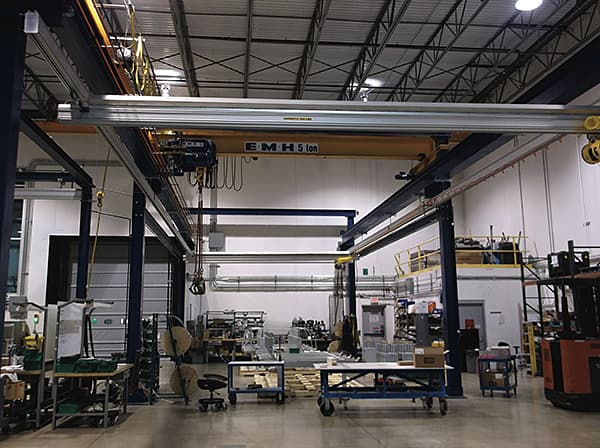
ABB is a global leader in power and automation technologies. For its US High Voltage Components Division in Mount Pleasant, Pennsylvania, ABB specified the EMH NOMAD® Free Standing Crane System, with capacities from 2-10 tons for shunt bank capacitor assembly–large and heavy units weighing 5 tons each and about 12 feet by 12 feet square by 6 feet tall.
The EMH NOMAD System was chosen based on cost, lead-time and compatibility to include another EMH product solution within the same floor space. EMH’s AL Systems™ Aluminum Crane Rail System, with capacities up to 2,200 lbs. was positioned directly underneath NOMAD to save valuable floor space, enabling 200 to 600 lb. pole mount capacitor assemblies in the same area.
Reliability was key. Once installed, both systems had to operate consistently without mechanical breakdowns. Then, after ABB consolidated facilities, both conveyor systems had to be disassembled, moved and relocated to another facility 10 miles away. Sometime after that, both systems had to be disassembled, moved and reassembled again, within the same facility with another 26 feet of rail length added. All installations were completed over the course of a weekend. All installations operated reliably, even after repeated application, saving ABB money.
ATC Provides Custom Assembly
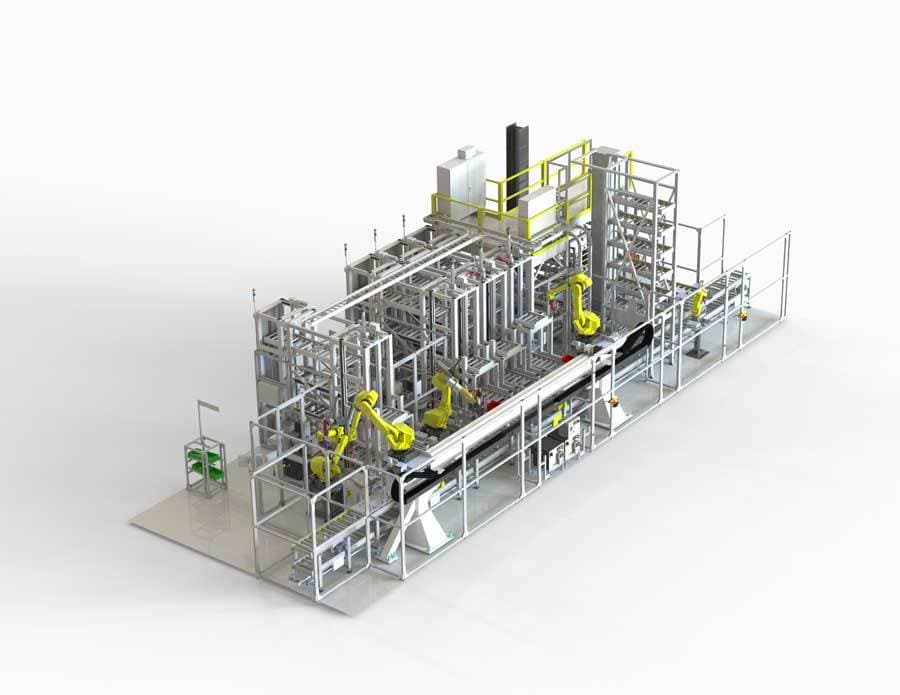
ATC Automation provides custom assembly and test systems for
the Transportation Business Sector. As the transportation industry continues its move to electrification, the demand for motor/stator assemblies has increased. Many traditional ICE tier suppliers are innovating with new electrification technologies. ATC automation has provided custom automated solutions for assembling and testing these electric vehicle systems for several customers. ATC’s experience with a long-time customer incorporates a non-synchronous assembly system with on-line manual assembly stations, semi-automated stations, and on-line automated stations. The project also included several off-line mini cells that feed the main assembly line.
The shaft and rotor assembly cell includes a close tolerance shaft press before moving the assembly to a magnetizer. A series of impulses at various heights and skew angles are used to magnetize the rotor. Flux density is then checked to ensure the proper level of magnetization has been achieved. Lastly, the magnetized rotor assembly is pressed into the housing on the non-synchronous main line.
The reject strategy for the cell is to route a reject to a repair cell. After determining the reject status, the assembly can be re-routed back through the assembly line to produce a finished quality assembly. To assure quality, the system utilizes a full traceability system to provide the finished product with a complete birth history.
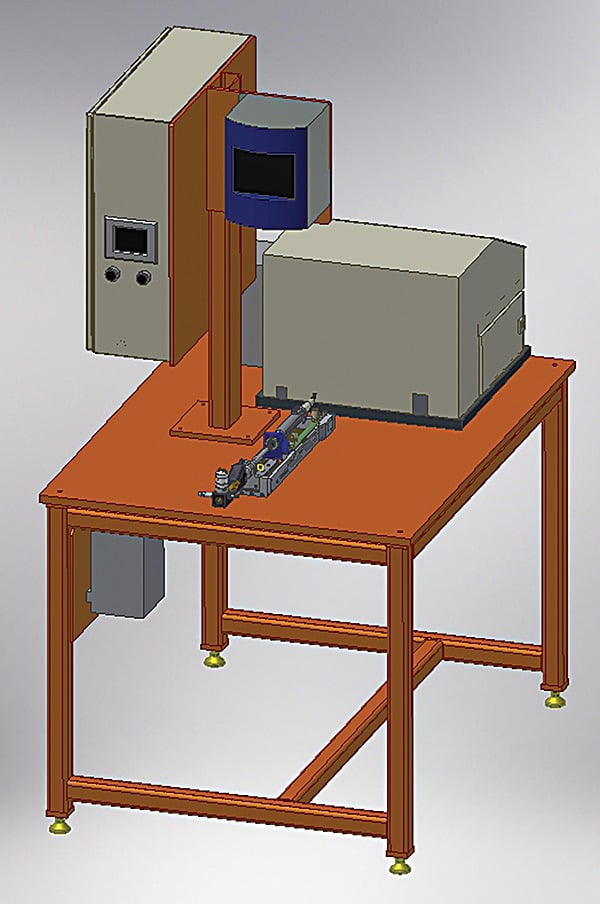
Installing a Valve Core with Perfection
An automotive tubing supplier partnered with Visumatic to develop an automated assembly machine to feed, lubricate, and install a valve core into a variety of vehicle charge port/tubing assemblies. Reaching a consistent target torque was historically difficult because the operator provided the tightening reaction force and sealing material made the joint dynamic. Physical reject control was also a concern because of the possibility of a bad part making its way back into the assembly stream.
Visumatic designed and built a simple solution to address these challenges. The process begins when the operator inserts the preassembled tubing/charge port into the fixture. Sensors initiate the assembly cycle as the fixture clamps the part in position. The Visumatic Power Module advances the valve core, the machine applies an aerosolized lubricant, and then installs it.
The force transfer to the operator was wiped out by the clamp mechanism, providing a stable environment for joint control. Tooling costs were kept low by identifying common locating features among the part styles resulting in a single fixture and no time consuming changeovers.
Passed part percentages were also increased through the incorporation of a DC electric driver motor with a programmed tightening sequence incorporating both target torque and angle. Rejected assemblies were controlled by retaining a failed part in the clamped fixture. Release of a bad part was only possible via a supervisor password lock-out accessed through the HMI.
Stop by our plant or visit our web site to see more Visumatic automated fastening in action.
Improved Valve Seal Installation Process
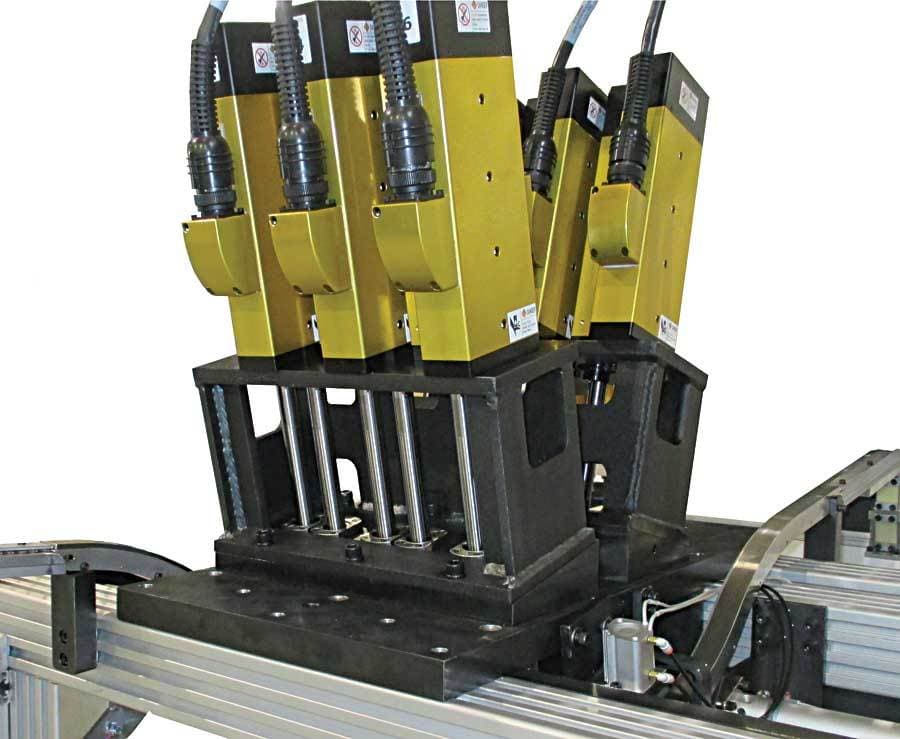
Challenge Issued – A major automotive manufacturer had previously used a single hydraulic cylinder to install/press cylinder head valve seals resulting in poor quality control, high scrap rates and no process data for birth history.
We were challenged to press the (12) valve seals into an engine cylinder head located on a cylinder head assembly line using a ‘small footprint’ press that would monitor the press process during the full insertion stroke and report final data for birth history.
Solution Given – FEC provided (12)-1KN “Mini” Series electric servo presses. The individual presses allowed independent seal insertion validation to proper load and distance specifications. A PC was provided for ease of press parameter programming and monitoring using the “No Cost” DSP3000 software provided with each press system. The PC also allowed press cycle result data and load/distance curves to be saved for birth history (sent to the plants SQL data server).
FEC is a full-service provider of fastening and pressing components as well as complete turn-key solutions to OEM and Tier 1 & 2 suppliers worldwide. Challenge Us.
Boulware Equipment, LLC
3134 Pinkie ln
Newton, NC 28658
704-651-6061
BRAD BOULWARE
PALLET TRASH, REPURPOSED FOR PROFIT
In 2017 Boulware Equipment commissioned the 1st of 2 Shredding systems at an assembly plant (pictured) in Eastern North Carolina. When the plant increased its capacity in 2018, they returned to Boulware Equipment for a 2nd Wood Grinding System. Now in 2021 both systems run simultaneously & Boulware Equipment is responsible for over 100 + Tons of Wood Scrap a week from this single location. This customer and many others choose Boulware Equipment for their wood scrap recycling solution because of how the scrap is handled & repurposed once it leaves your plant. Boulware Equipment provides turn-key equipment design, installation & startup. Our network of 100s of wood fiber buyers across the USA allow us proudly to say we NEVER take wood scrap to the landfill.
Our company supplies woodchip trailers and logistics for the wood fiber recycling at no charge to our customer. We reduce costs, lower your carbon footprint, and repurpose your wood trash in a responsible way, and guarantee no landfill. Repurposing wood trash is our mission.

Universal Robots USA, Inc.
5430 Data Court, Suite 300
Ann Arbor, Michigan 48108
United States
844-462-6268
Cobots Automate Small Batch Welding
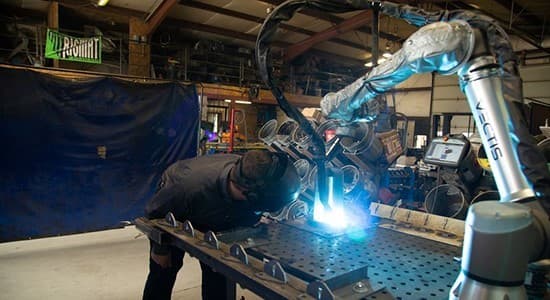
MT Solar, based in a remote area of Montana, designs and manufactures mounting structures for solar modules of all sizes. The company’s lead times were two to three times what they were supposed to be due to labor challenges. “It’s hard to find good, skilled people that are willing to come up here and work,” explained MT Solar owner and president Travis Jordan.
His hiring woes reflect a national trend; the American Welding Society predicts a potential shortfall of 400,000 welders by 2025. MT Solar researched conventional welding robots but found them best suited to huge batches of the same item and lacking in flexibility. Finding a flexible automation solution was crucial for MT Solar as the company makes many different types of mounting parts, often in high mix/low volume batches.
After discovering collaborative robots from Universal Robots, the paradigm changed. MT Solar implemented the Vectis Automation’s Cobot Welding Tool powered by Universal Robots, which now handles a wide range of welds, enabling quick change-overs and optimized production, and they now have the ability to meet 300% seasonal increase in demand without hiring extra staff.
DEPRAG
640 Hembry St.
Lewisville, TX 75057
800-433-7724
972-221-8731
A Step Up from Vibratory Bowl Feeding!
The eacy feed systems have it all – efficiency, assembly, communication, yield. Ideal for the smart factory/Industry 4.0, the 24 V drive enables a wide array of applications, all while delivering approximately 80% power savings. The revolutionary eacy feed makes stationary and manual assembly easy – from screws, nuts, and threaded pins to o-rings, parts for cleanrooms, and more.
Now, even the feeding of large screws is no problem with the new DEPRAG eacy step feed system that is fast, efficient, and exceedingly gentle to long fasteners while incorporating all the other well-known eacy feed features.
Even better, eacy feed also feeds information. Production managers benefit from best-in-class technology that delivers essential feedback and information such as productivity & efficiency of operators, maintenance requirements, and much more. The vibratory- and step feeding system of the future, eacy feed makes transportation of fasteners easy.
Efficiency – approximately 80% reduced power consumption.
Assembly – optimized for user-friendly operation.
Communication – perfect for the Smart Factory / Industry 4.0 automated environment.
Yield – modular components and advanced design deliver
reliable performance.
DEPRAG USA is located near Dallas, Texas, providing Canada and the Continental U.S. with quality screwdriving equipment and excellent service.
DEPRAG combines over 88 years of experience and more than 40 years of feeding technology with sophisticated, cutting-edge technology.
To learn more about the eacy feed systems, contact DEPRAG today.

August 2021
Scroll to
read full story